How a Custom FRP Part Moves from Drawing to Finished Assembly
Follow the decisions and checks behind custom fiberglass tooling, molding, trimming, finishing, first-article approval and protected delivery.
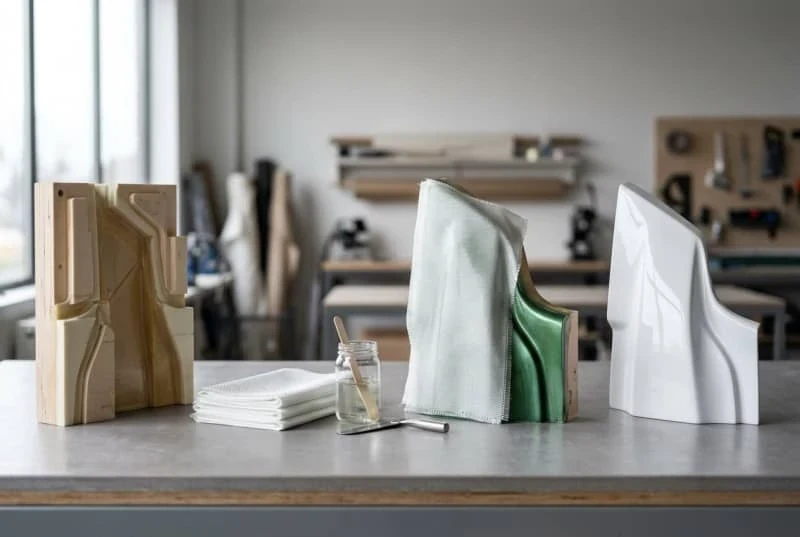
A custom FRP component passes through drawing review, tooling, molding, trimming, finishing and inspection. The exact route depends on its geometry, construction and quantity. Ask the manufacturer to describe the proposed process for your part and the approval record at each stage.
The drawing, material requirements and finish reference should describe one configuration. Keeping them aligned prevents a correctly molded surface from reaching assembly with the wrong opening, hardware or joint.
1. Review the part and its mating assembly
Provide a surface model or dimensioned drawing, equipment references and the required loads, exposure and finish. Identify dimensions that control fit, surfaces visible after installation and areas the supplier may revise for manufacture.
For an FRP dashboard shell, the review needs the instrument layout, support frame, device openings and service access. Confirm what is supplied with the shell and what remains with the vehicle assembly team. A smooth exterior model alone cannot establish the fit behind the instrument face.
The manufacturability review should propose mold splits, release access, trimming allowances and part divisions. Resolve undercuts and hardware zones before the tooling geometry is approved.
2. Agree the pattern and mold strategy
The tooling route may use a master pattern, temporary prototype tooling or production molds suited to the chosen process. Agree which route the quotation includes, the intended quantity and any corrections required after the first trial.
Review the tool surface against the approved model, particularly visible contours and adjoining component edges. Identify which dimensions are formed by the mold and which are created later by trimming or machining. Mounting holes and cutouts need their own datums and inspection method.
Record tooling ownership, storage and maintenance arrangements. For a multi-part shell, keep the mold and component identifiers connected to the assembly drawing.
3. Mold the agreed construction
The manufacturer selects a process and laminate construction for the released part. The proposal should identify the resin and reinforcement requirements, local reinforcement, any core or inserts, and the applicable process controls. Hand lay-up, vacuum-assisted or closed-mold routes have different tooling and production needs; none should be selected only from the component's appearance.
Discuss the checks that matter to the part: material identification, reinforcement placement, local thickness and the defined cure requirements. Where loaded hardware or bonded components are included, agree their construction and inspection before producing the sample.
A finish requirement also affects this stage. Mold-surface condition and reinforcement transitions influence the surface that later finishing operations must accept or correct.
4. Trim openings and fit hardware
After release from the mold, edges, access openings and attachment features are completed to the drawing. The manufacturer needs consistent references for locating these features, particularly where the part meets a separately supplied frame or device.
A laboratory analyzer housing needs device-mounting datums, connector clearance and removable panel access. Check the equipment installation and removal route with the selected hardware fitted. An opening that measures correctly can still obstruct a cable or component during maintenance.
Agree how inserts, hinges, seals and fasteners are supplied. Identify any loose parts and assemblies that the buyer installs after delivery.
5. Finish the specified surfaces
The finishing scope may include a molded surface, local preparation or a separate coating system. Set the accepted color, gloss, texture and edge treatment with a physical sample. Define visible faces and viewing conditions so appearance is judged consistently.
For a dental unit cover, include contact edges, panel joints and the specified cleaning exposure in the finish review. Approve the proposed surface against the device requirements; the cover's appearance does not establish clinical or system-level acceptance.
Record acceptable repair methods and any areas where repair marks are restricted. Keep the accepted finish sample available for production inspection.
6. Approve the first article and release the batch
Use an inspection report to connect the sample with its drawing revision. Check critical dimensions, hardware operation, mating fit and finish, then perform any specified application tests. Identify who approves each result and how sample comments are closed.
When a correction changes tooling, construction or an interface, update the released record and repeat the affected checks. Production should follow the accepted configuration, not a mixture of the original model and later informal instructions.
7. Protect and identify the finished components
Specify packing supports, contact protection and restraint for projecting returns or finished faces. Label different panels and loose hardware against the assembly schedule. Confirm packed dimensions, handling points and unloading access before dispatch.
Request the agreed shipment records, such as drawing revision, part quantities and inspection results. On receipt, check component identification and visible condition before unpacking the assembly for installation.
Keep reading
More from the FRP journal
What Fiberglass Is and What to Specify for Custom FRP Parts
Define geometry, loads, exposure, finish and acceptance criteria when ordering custom fiberglass components for buildings, equipment and public spaces.
Specifying Fiberglass Components for Outdoor Exposure
Plan outdoor FRP components around weather exposure, mounting details, finish samples, packing and maintenance requirements.
Reducing FRP Part Weight Without Losing Required Performance
Set a complete-assembly weight target, protect mounting and service interfaces, and verify custom FRP parts through sample weighing and application-specific checks.